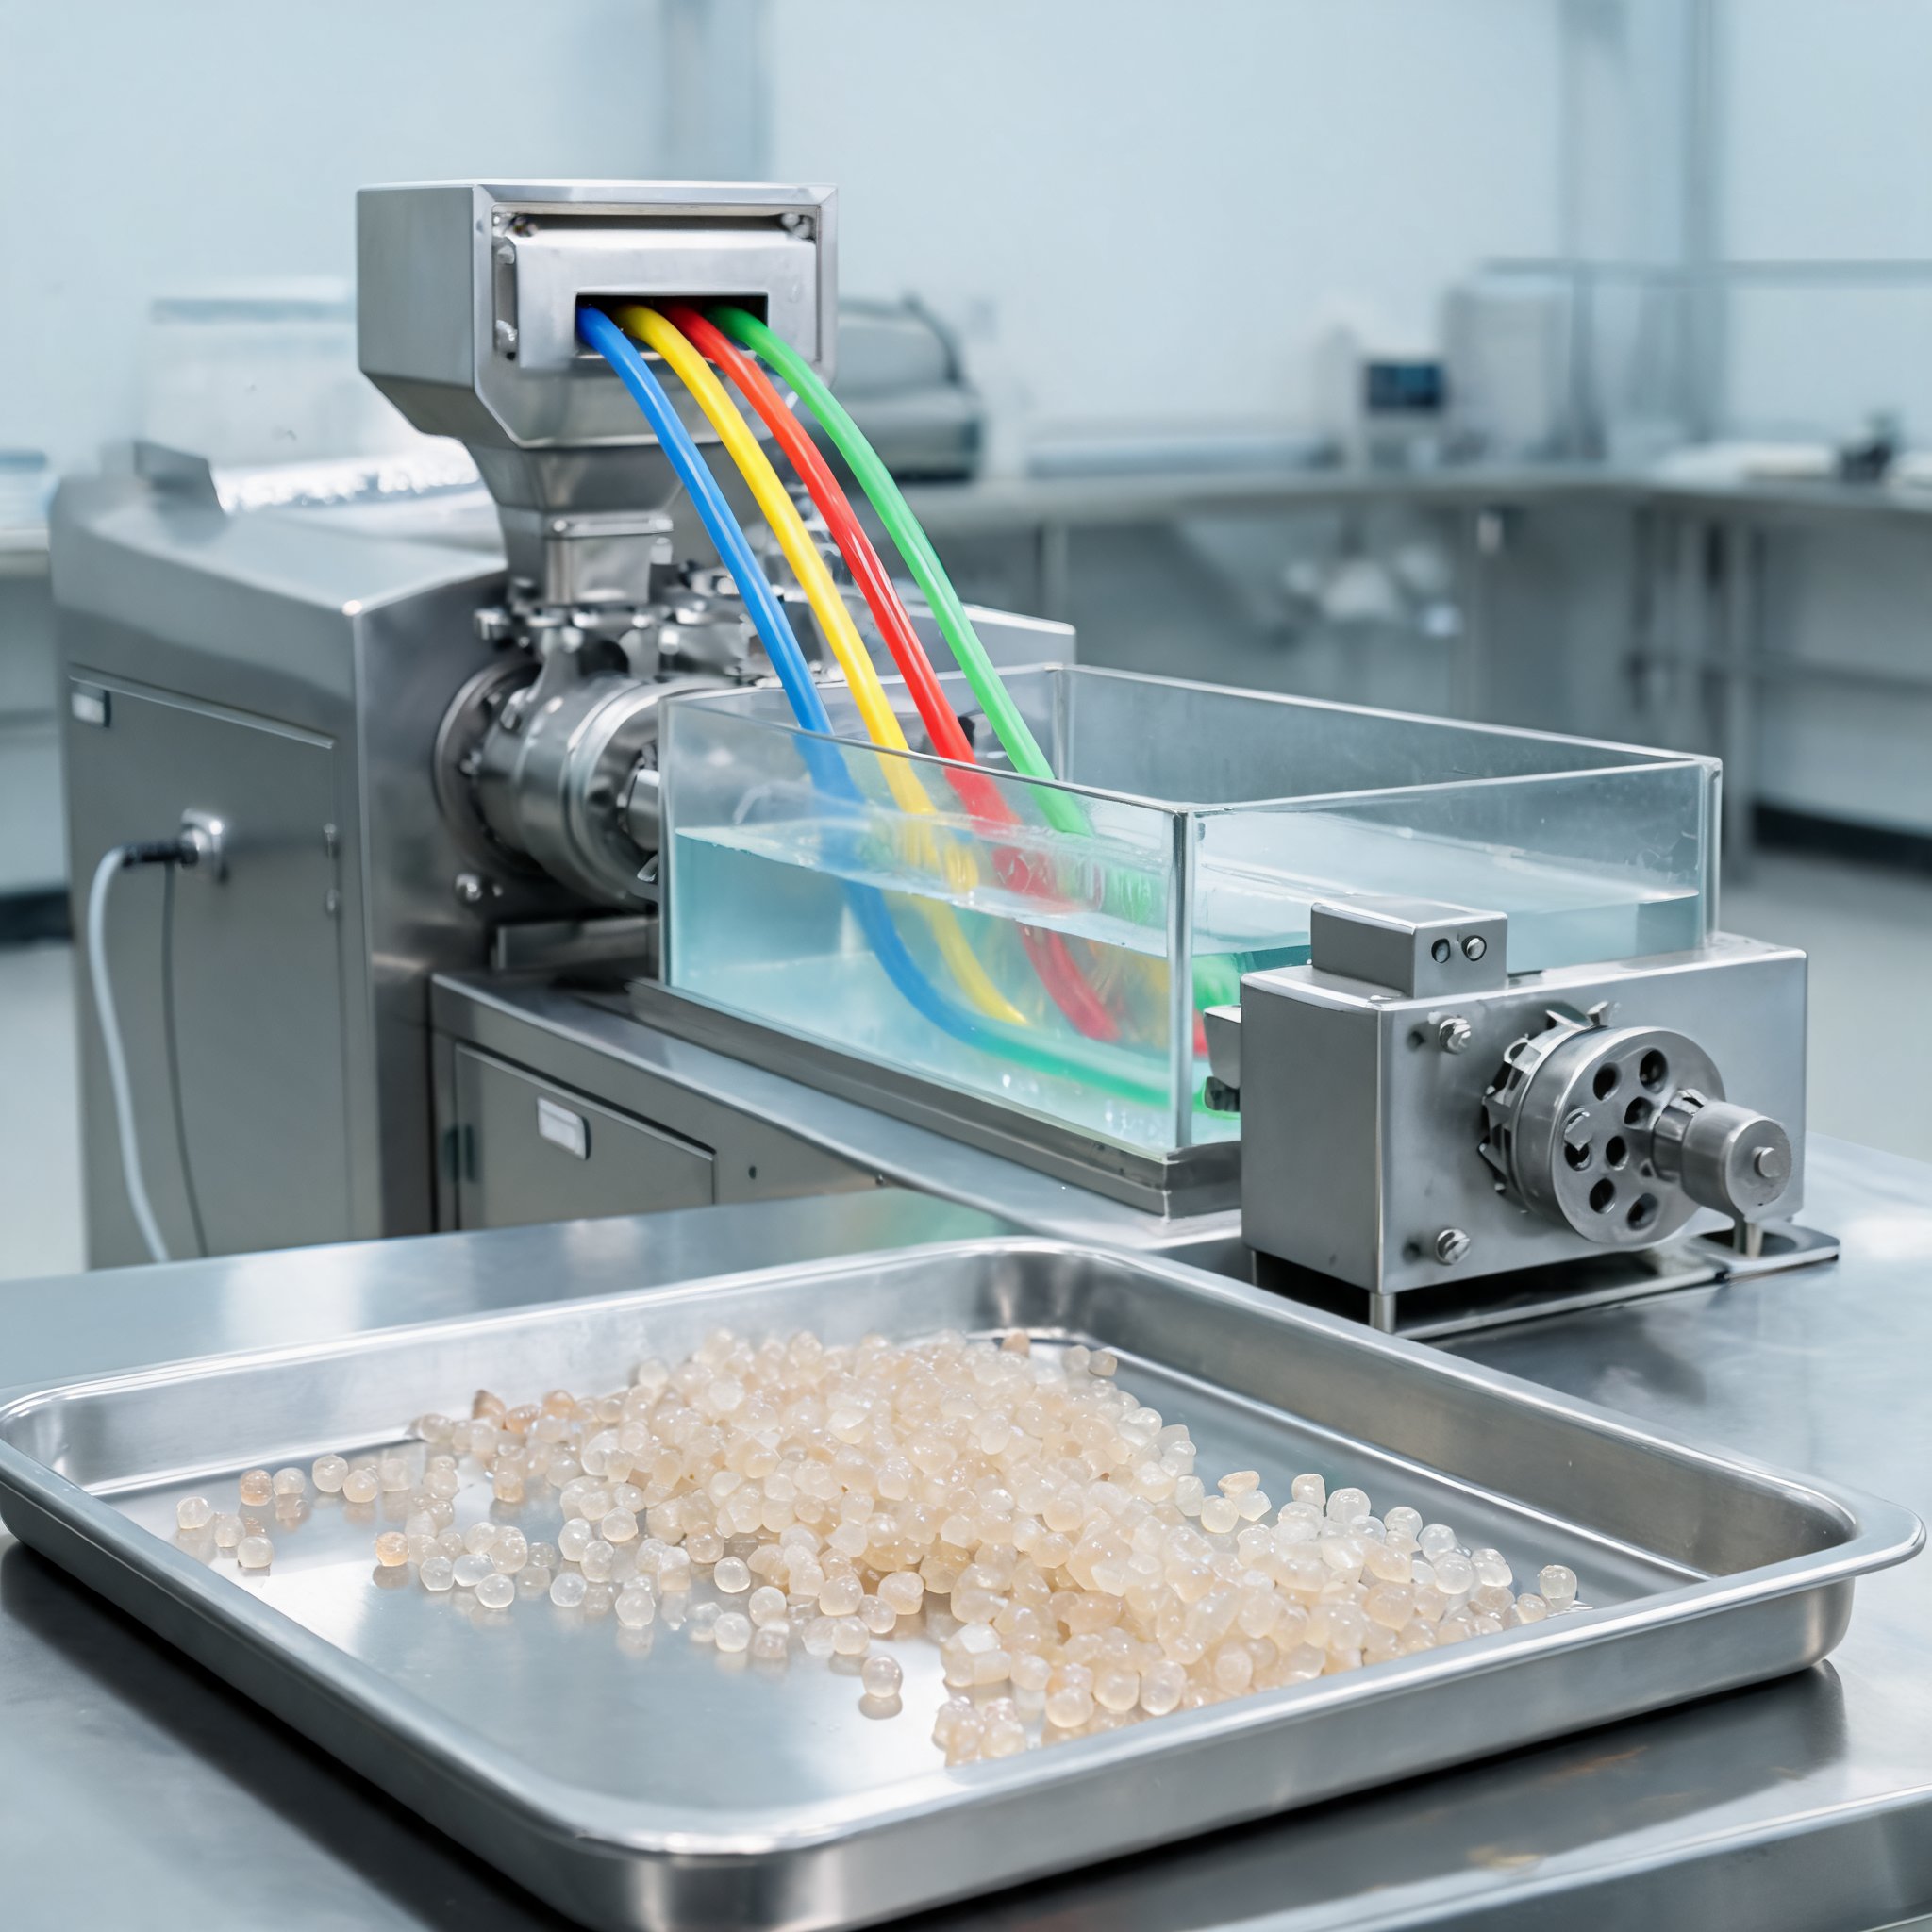
Researchers have examined whether four commercial natural colorants can be carried through industrial melt processing in two biodegradable polyesters without losing their color or degrading the surrounding polymer. The study, titled Sustainability in the Development of Natural Pigment-Based Colour Masterbatches and Their Application in Biopolymers, produced color masterbatches by twin-screw extrusion and then diluted them into the matching polymer matrix at 2, 4 and 6 wt% to make injection-molded test specimens.
The pigments examined were blue spirulina, yellow curcumin, red beetroot and green chlorophyllin. The masterbatch formulations also contained titanium dioxide, calcium carbonate and stearic acid, which were included to support UV protection, pigment dispersion and processing.
Processing window shaped by pigment degradation
Heat is the central difficulty when natural colorants meet melt processing, because their organic structures can begin to break down at lower temperatures than the polymers they are meant to color. Thermogravimetric analysis placed degradation onset at roughly 229 °C for spirulina, 244 °C for curcumin, 258 °C for chlorophyllin and 267 °C for beetroot. PLA and PBS were found to degrade at considerably higher temperatures.
The team therefore set extrusion profiles that melted each polymer while limiting the thermal load on the pigments. Processing temperatures reached 145 °C for PBS and 190 °C for PLA, with the twin-screw extruder running at 65 rpm and a feed rate of 2 kg/h.
That window suited most pigment–polymer pairings, with spirulina as the clear exception. During PLA processing the spirulina lost its characteristic blue, so a blue PLA masterbatch could not be produced. In PBS, the lower processing temperature left enough pigment stability for compounding to succeed. The result indicates that pigment compatibility is closely tied to the thermal demands of the specific matrix.
Melt flow and mechanical values stay near baseline
From a processing standpoint, the natural pigments caused only limited shifts in rheology. Melt flow rate fell slightly after incorporation, pointing to a modest rise in melt viscosity. Neat PLA measured about 50 g/10 min, and the corresponding natural-pigment masterbatches remained close to that figure. PBS responded in a similar way, with only a minor reduction.
The researchers note that this matters for compounders: a natural color system has little practical value if it forces major revisions to screw design, pressure settings or molding conditions. In this work, conventional twin-screw compounding and injection molding handled most formulations without significant problems.
Tensile and impact behavior were also checked across the 2 to 6 wt% addition range, and neither polymer showed meaningful overall losses. PLA began at a Young's modulus of about 1710 MPa and a tensile strength of 65.6 MPa, while PBS began at about 392 MPa and 34.5 MPa. The colored formulations stayed close to those baselines. Impact strength remained in a comparable range, although individual pigments introduced some variation.
Color retention under light is the largest obstacle
Successful extrusion did not guarantee durable color. After 50 hours of xenon-lamp exposure, most formulations exceeded a color difference of ΔE* = 2, a level generally taken as a visible change. The PLA formulation containing 2 wt% green chlorophyllin masterbatch was the main exception, showing the highest photostability.
The authors therefore identify UV stability as the biggest barrier to wider adoption. Packaging, consumer goods, agricultural parts and outdoor applications may need extra stabilization, protective coatings or pigment modification before natural colors can match conventional systems over long service periods.
Lower carbon footprint in the study's comparison
The environmental comparison favored the natural route under the study's assumptions. One kilogram of curcumin pigment was associated with about 0.04 kg CO2-eq, against 18.65 kg CO2-eq for the inorganic green reference pigment. The natural-pigment masterbatches also used less electricity during extrusion and pelletizing.
The researchers conclude that natural pigment masterbatches still need work, particularly on lightfastness and thermal stability. Even so, the study shows that several natural colorants can be compounded into PLA and PBS on conventional equipment with only limited changes in melt viscosity and mechanical performance. Future efforts, they suggest, should target color stability both during processing and during subsequent service exposure.